Monday to Saturday - 8:00 -18:00 (CET/CEST)
Okuma 2SP Series Repair & Support
Diagnostics and repair for Okuma’s front-facing, parallel twin-spindle lathes — the 2SP-150H, 2SP-2500H and 2SP-35H, purpose-built around gantry-loader automation for mass production.
What Is the Okuma 2SP Series?
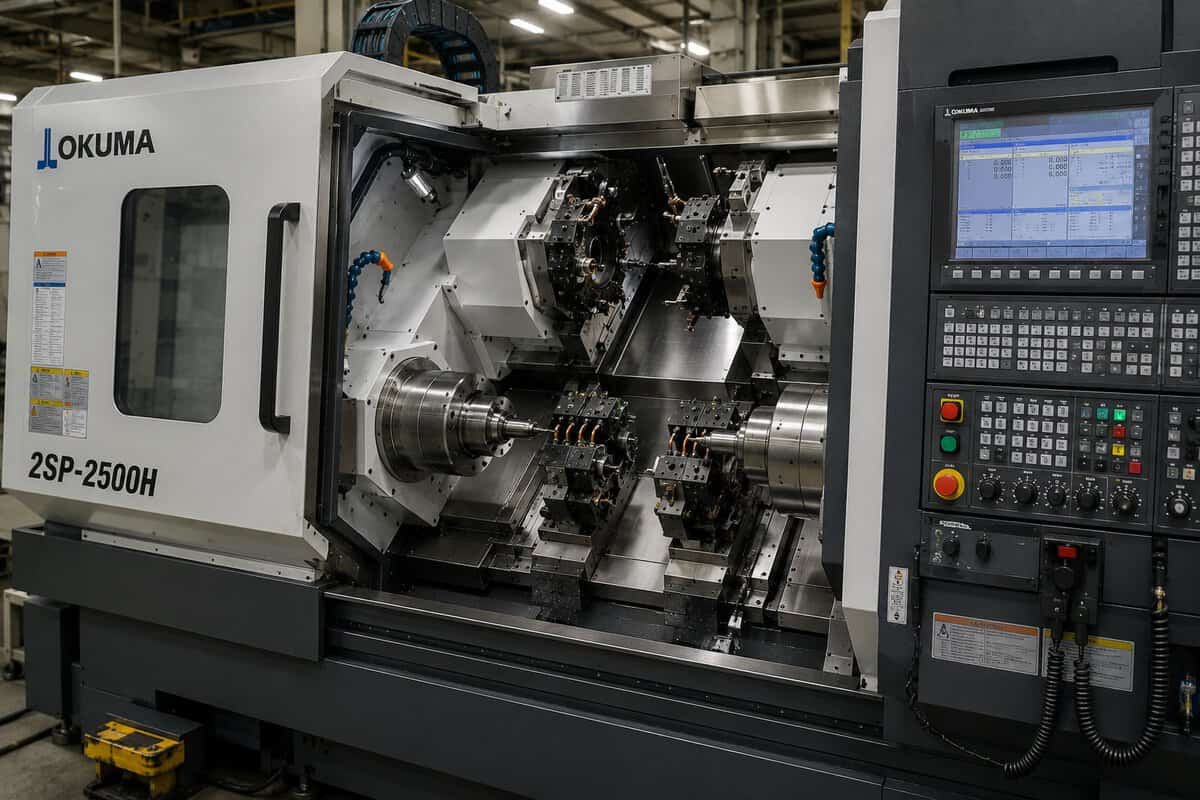
The 2SP Series takes a different approach to twin-spindle production than any other Okuma lathe on this site. Rather than a sub-spindle behind the main spindle (LB Series), a front-and-back part transfer (TWIN STAR LT), or a mirror-image second lathe under one control (2SP-V), the 2SP-H machines mount their spindles side by side, facing forward. That front-facing layout exists for one specific reason: it makes the machine exceptionally easy to automate. Because the spindle sits off to the side rather than in the traditional position, an Okuma Gantry Loader can enter and load or unload a part regardless of where the turret currently is — there’s no need to retract the turret out of the way first, which is exactly the kind of small mechanical detail that adds up to real cycle-time savings over a production shift. Okuma classifies this line under “Parallel Spindle CNC Lathes” in its own product catalog, a distinct category from the twin-turret and twin-spindle-transfer lathes covered elsewhere on this site.
The result, on the 2SP-2500H specifically, is a 4-second chuck and unload cycle and a machine width of just 2,200mm — the smallest footprint in its class — while still handling parts up to 250mm in diameter. Okuma markets the 2SP Series specifically for mass-production automotive parts, where the combination of two independent spindles, fast automated loading, and a compact footprint lets a shop run two effective lathes’ worth of output from roughly one lathe’s worth of floor space. For shops weighing up whether to add a second standalone lathe or consolidate into one 2SP machine, the floor-space savings alone are often the deciding factor.
Milling capability is optional across the range but genuinely capable when fitted — the 2SP-2500H’s optional milling motor output was doubled in its most recent update, putting its face-milling, drilling and tapping performance close to that of a small dedicated machining center, on top of its core turning work.
2SP Series Models & Specifications
The three current 2SP-H models scale from small precision parts up to mid-size automotive components, all sharing the same front-facing, parallel-spindle architecture.
2SP-150H
- Max. turning diameter: 220 mm
- Max. turning length: 150 mm
- Tool stations: 2 x 12
- Compact class for small precision parts
2SP-2500H
- Max. turning diameter: 250-410 mm
- Max. turning length: 200 mm
- Spindle speed: up to 5,000-6,000 min⁻¹
- Motor: 2 x 15/11 kW · optional milling (up to 7.1 kW)
- Gantry Loader (OGL) standard integration
2SP-35H
- Max. turning diameter: 380 mm
- Max. turning length: 230 mm
- Tool stations: 2 x 12
- Larger-part class within the 2SP-H range
Shared Design Features
- Front-facing spindles, mounted side by side
- Centrally aligned spindles and turrets on a box-way guide
- 4-second chuck/unload cycle (2SP-2500H)
- Thermo-Friendly Concept thermal stability
All three models share the same fundamental layout — two parallel spindles, front-facing for loader access, on a rigid box-way guide system — scaled to different part sizes. The “M” feature code indicates milling tools are fitted to the turret; without it, the machine is turning-only.
Which OSP Control Does the 2SP Series Use?
Current 2SP-H machines run Okuma’s OSP suite with pre-loaded automation applications specifically aimed at gantry-loader integration — the control isn’t just running the lathe, it’s actively managing the handshake with the loader on every cycle. Depending on the machine’s age, that’s typically OSP-P300 or a newer generation.
Because loader timing is baked so deeply into the control logic on this platform, confirming the exact OSP version and automation application configuration matters more here than on a standalone lathe without integrated automation — two 2SP-2500H machines running different OSP versions can behave differently with the same loader hardware, even when the mechanical loader setup itself is identical.
Common 2SP Series Faults We Repair
The 2SP Series’ front-facing, automation-first design creates a fault profile centered on loader integration and dual-spindle independence.
Front-facing spindle drive faults
The side-mounted, front-facing spindle arrangement doesn’t change the fundamentals of spindle drive diagnosis, but it does change access — on a 2SP machine, we treat each spindle’s drive and encoder as an independent diagnostic path from the start, since the two spindles’ compact side-by-side mounting means a fault on one can be mistaken for a fault on the other during a quick visual check.
Gantry loader (OGL) integration faults
Because the OGL is designed to enter regardless of turret position, faults here tend to be handshake timing issues, gripper faults, or loader-to-control communication errors rather than a mechanical turret-clearance problem. This is the single most common fault category we see on 2SP machines, simply because loader integration is so central to how the machine is meant to run — a shop that’s only used stand-alone lathes before may not initially think to check the loader interface as a first step, when on this platform it’s often exactly where the fault lives.
Twin parallel spindle synchronization faults
Where both spindles are meant to run mirrored or coordinated cycles for maximum throughput, timing drift between the two shows up as one side finishing noticeably ahead of or behind the other. This is usually a drive-tuning difference between the two spindles rather than a control-level synchronization fault.
Milling and turret faults (M-equipped machines)
On machines with the optional milling package fitted, indexing faults and milling-spindle drive issues follow standard turret-repair patterns, but given the higher motor output on milling-equipped 2SP-2500H units, thermal protection trips during heavy face-milling are worth ruling out before assuming a genuine drive fault.
Display and operator panel faults
Standard OSP panel and display faults follow the same repair pattern as other Okuma lathes.
Given how central automation is to this platform, we always check the loader handshake and both spindles’ independent electronics before assuming a fault is isolated to a single component. See our fault analysis and testing & diagnostics services for more on our approach.
Components We Repair on the 2SP Series
Given the 2SP Series’ automation-first, twin-spindle design, these are the parts we’re asked to repair most often:
Spindles
Independent left and right front-facing spindle drive repair.
Control Boards
OSP board repair, including loader-automation application logic.
Gantry Loader Interfaces
OGL handshake, timing and gripper fault diagnosis.
Servo & Spindle Drives
Dual-spindle drive electronics repair and synchronization tuning.
Turrets & Milling Tools
Turret indexing and optional milling-spindle repair.
Operator Panels & Displays
CRT, LCD and touchscreen repair for OSP control panels.
2SP Series Repair Services
The following services apply directly to 2SP Series machines, whatever the fault:
CNC Control Repair
Board-level repair, including automation application logic.
Drive Units Repair
Component-level repair of dual-spindle drive electronics.
Testing & Diagnostics
Practical fault diagnosis before any repair work begins.
Spindle Repair & Maintenance
Service for both front-facing spindle sides.
Emergency & Express Repair
Priority turnaround with loaner units to minimize downtime.
Retrofit & Modernization
Upgrade path for older 2SP machines running legacy controls.
Industries That Rely on the 2SP Series
Built for compact, fully automated mass production, the 2SP Series shows up most often in:
Where We Support 2SP Series Machines
CNC Elektronik is based in Germany, where mass-production automotive parts manufacturing makes the 2SP Series a common sight on shop floors we work with regularly.
We’ve also supported 2SP Series repair work in Brazil, where automotive component manufacturing benefits from the same compact, automated twin-spindle setup. The repair process is the same regardless of distance: isolate whether the fault is in a spindle, the loader interface, or the control’s automation logic, repair or replace the failed component, and confirm the machine — loader included — is running correctly before it returns to production. Because these machines are typically running as part of a fully automated, unattended production cell, an unresolved fault often means the whole cell sits idle rather than just one machine, which is why a fast, correct diagnosis matters even more here than on a manually operated lathe.
See our Countries We Serve page for our full regional coverage across Europe, the Americas, and parts of Asia and the Middle East.
Explore More Resources
The 2SP Series is one part of a much wider Okuma ecosystem. Here’s where to go next:
All Okuma Models
Browse every Okuma machine series and model we repair.
OSP Controls
Every OSP control generation we diagnose and repair.
Automation & Robotics
Every gantry loader and automation type we support.
Components & Parts
Every part type we repair, across the full Okuma range.
Countries We Serve
Where our repair and support coverage extends to.
Spare Parts
New and used Okuma electronics spare parts, tested before sale.
Frequently Asked Questions
The model number is printed on the machine’s nameplate, and the OSP control generation shows on the control cabinet nameplate or startup screen. Send us a photo of either and we’ll confirm it.
The 2SP-H Series covered here is a horizontal, front-facing parallel-spindle lathe built for small mass-produced parts with gantry-loader automation. The 2SP-V variants are vertical lathes for large, thin, odd-shaped parts like aluminum wheels. Despite the shared “2SP” prefix, they’re built for very different part types.
Yes. Because the OGL is so tightly integrated into how the 2SP Series operates, we treat loader diagnosis as a core part of the repair rather than a separate add-on service.
Usually not. We diagnose each spindle’s drive and encoder independently, so a fault on one side typically doesn’t require disturbing the healthy spindle’s electronics.
In most cases, yes. Component-level repair of a control board, spindle drive or loader interface is almost always far cheaper than replacing a fully automated production cell, and the platform’s compact, rigid construction is built for long service life.
Yes. The milling motor, turret drive and associated tooling on M-equipped 2SP-2500H machines fall under the same turret and drive repair services we provide for the core turning function.
Have a 2SP Series Issue?
Send us your model number, control type and a description of the fault — we’ll get back to you with a practical assessment.